Technical Notes
Solvent TIJ Cartridge on Metal, Glass & Plastic: Adhesion Guide
Adhesion on metal, glass, PET and PE/PP film fails for five different reasons, and the cartridge is rarely the variable. What goes wrong on each substrate, what to check before a trial, and how to judge drying and adhesion on your own line.
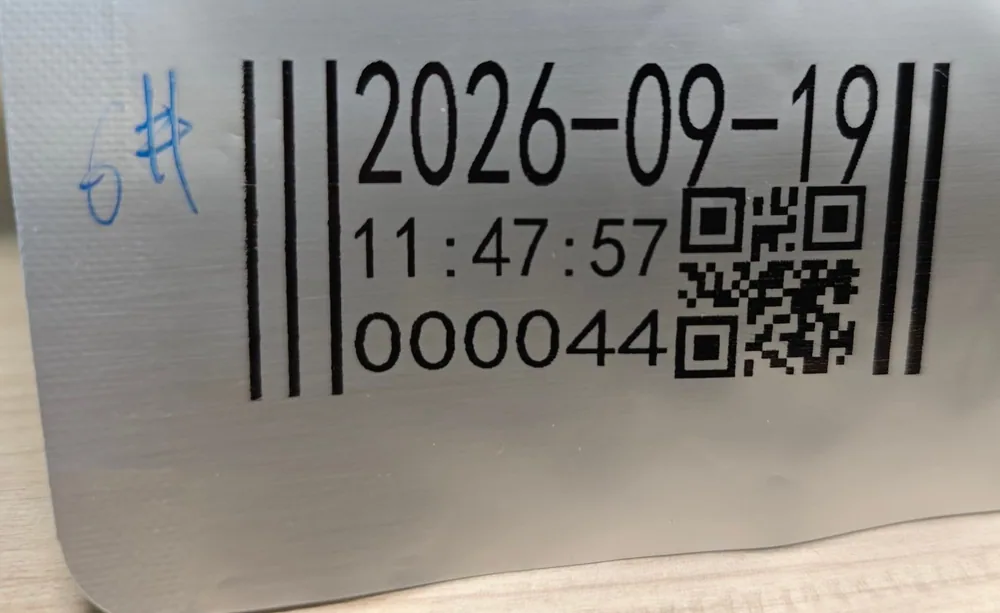
A solvent TIJ cartridge prints well on metal, glass and plastic — and fails on exactly the same three materials, for different reasons. The cartridge is usually not the variable. The surface is.
That is the first thing to get straight before ordering. A solvent TIJ cartridge (TIJ, thermal inkjet) is a 42 ml HP45-format cartridge with fast-dry solvent ink, built for non-porous surfaces where water-based ink beads up and wipes off. Our XM-45S prints at a native 300 dpi, up to 600 dpi depending on print mode, in 12.7 mm and 25.4 mm print heights. It dries typically in 1–5 seconds on non-porous surfaces — but “typically” is doing a lot of work in that sentence. On a clean aluminium can it may be dry before the next roller; on a cold glass bottle, a silicone-treated PET bottle or an untreated PE pouch, the same cartridge can smear, flake or refuse to wet at all.
The short answer: the cartridge is the same in all five cases. What differs is the surface, and the only evidence that counts is a print on your own product at your own line speed.
For each of the five common substrates this guide covers four things: what usually goes wrong, what to check before a trial, how to tell whether drying is good enough, and what to do when the print fails. Every section ends in the same place — print on your own product, at your own line speed, and judge the result there.
If you want the surface-energy numbers, pretreatment thresholds and test standards first, read the substrate matching guide: dyne levels, corona and flame treatment, ASTM references. And for what a solvent cartridge is and when to choose it over aqueous or UV, see the pillar guide, What Is a Solvent TIJ Cartridge?.
Before any substrate: three checks that apply to all five
Most adhesion failures are diagnosed faster by checking these three things first, before blaming the ink or the cartridge.
1. Is the surface clean, dry and at room temperature? Dust, forming oil, mould-release residue, fingerprints and condensation all sit between ink and surface. Solvent ink tolerates more contamination than aqueous ink, but it cannot bond through grease. A cold-filled bottle in a warm hall grows condensation; ink printed onto water will not bond. Code glass before filling, after it reaches room temperature, or where the surface stays dry.
2. Is the printhead close and steady? The optimum throw distance is 1–2 mm, usable up to 5 mm with loss of placement accuracy. A wobbling conveyor, a curved bottle shoulder or a pouch that flutters can move the surface out of range and blur the print. Fix the handling before changing the ink.
3. Where does the code first get touched? Drying time only matters in relation to what happens after the printhead: the first roller, the first stacker, the first time two printed surfaces touch. Measure that distance and your line speed — those two numbers define the drying budget. Where the budget is too short, the options are to move the printhead, add an air knife or dryer, reduce the ink load, or change the ink system. Changing the cartridge alone rarely fixes a drying problem caused by line layout.
How to judge every trial the same way
Judge every trial the same way, in this order: tape test (apply pressure-sensitive tape, press firmly, remove at 90 degrees, look at how much ink lifts), wipe test (ethanol or IPA as used in your cleaning process, wiped under consistent pressure), rub test (count the double rubs to breakthrough rather than recording a pass or fail), then an environmental check (cold store, condensation, alcohol contact — whatever your product actually meets) and a scan test with the equipment you will use at end of line. Print the sample at your line speed with your real code content. A coupon printed in a lab is not evidence about your product.
A pass on a flat coupon is the weakest evidence in this whole process: it tells you the ink can bond to something, not that it bonds to your part under your conditions. Count the rubs rather than ticking a box, because “passed” hides the difference between a code that survived four double rubs and one that survived forty — and the first one is the one that fails in transit.
The five substrates at a glance
| Substrate | Usual failure | Check first | Drying watch-out |
|---|---|---|---|
| Metal (aluminium, tinplate, coated steel) | Print wipes off forming oil or lacquer | Oil, coating type, lacquer | Usually forgiving once clean; cure, not just dry-to-touch |
| Glass | Condensation under the ink; primer-dependent adhesion | Temperature, condensation, primer | Code before filling or at room temperature |
| PET and rigid plastic | Slip agents, silicones, anti-static coatings | Surface treatment, supplier batch | Fast, but check rub resistance after cure |
| PE and PP film | Low surface energy; ink beads and flakes | Dyne level, corona treatment, film movement | Film flutter moves the surface out of range |
| Coated carton | Coating behaves like plastic, not paper | Coating type (matte vs glossy UV) | Test both ink types if the coating is unknown |
Each row below is adhesion by substrate expanded in the same four parts: what usually goes wrong, what to check before a trial, how to judge drying, and what to do if it fails.
Metal: aluminium, tinplate and coated steel
Metal is usually the most forgiving of the five — which is why a failure here is worth investigating rather than accepting.
What usually goes wrong. Forming oils on cans, caps and foil seals; a lacquer or varnish coating that becomes the surface you are actually printing on. A lacquered metal behaves like the lacquer, not like the metal. If prints wipe off, clean a sample and print again before blaming the ink — residue is the more common cause.
Check before a trial. What is the coating, if any — bare metal, lacquer, varnish, anodised layer? Has the part been handled, oiled or stored in a way that leaves a film? Is the surface flat and stable at the print point, or curved enough that the throw distance varies across the code?
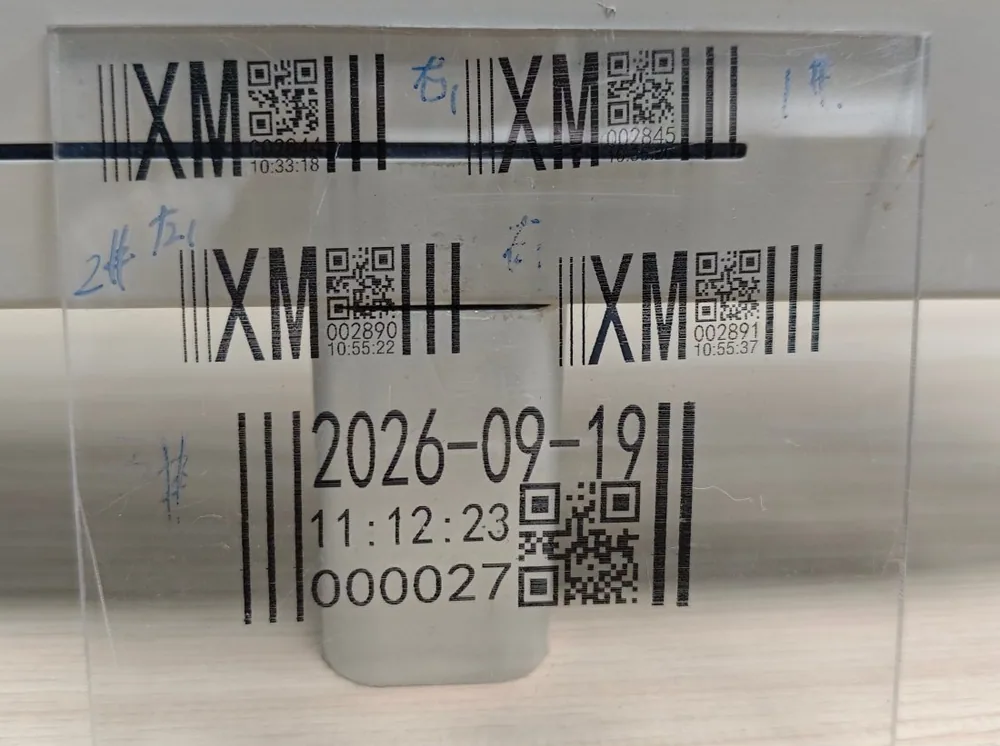
How to judge drying. A test print on an aluminium plate — date, time, serial number, barcode and QR code — is the reference case for this cartridge. The code should be dry to handle within the usual 1–5 second band, but do not stop there: cure is not the same as dry-to-touch. If the code is wiped or abraded immediately after printing, it can be removed while it still looks set. Allow for the cure time in the line layout, and rub-test after the product has reached the first point where it is handled or stacked.
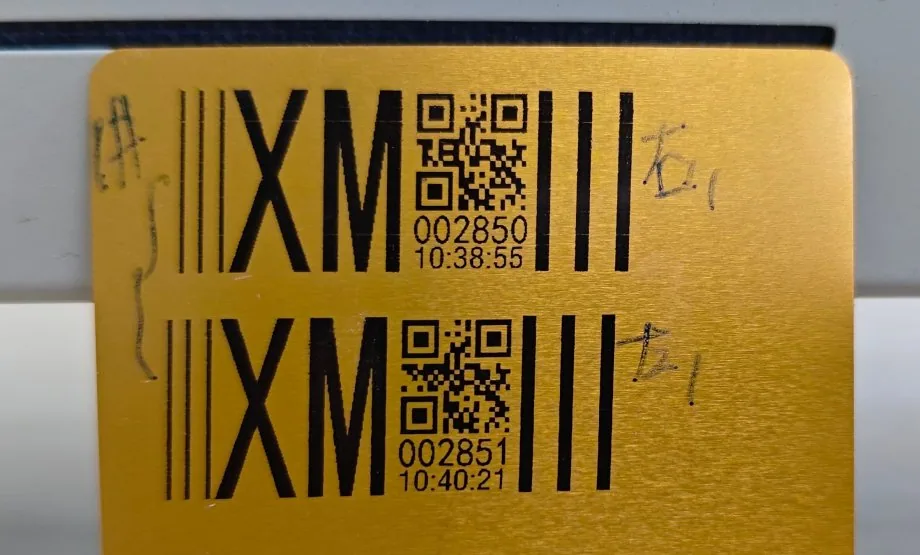
If it fails. Clean the sample and retest; if it still fails, check the coating rather than the ink. A different lacquer from a different supplier can change the result with the same cartridge, so test the actual supplier batch, not a generic metal coupon.
Glass: bottles and jars
Glass prints well, but it adds temperature — and temperature is usually the failure, not the glass.
What usually goes wrong. Condensation on cold-filled glass, and adhesion that depends on a primer rather than on the ink alone. Glass has high surface energy but is chemically inert, so the ink has little to grip chemically. A code that looks perfect on a warm, dry bottle can fail on the same bottle straight out of the filler. Geometry compounds it: on a curved bottle the throw distance varies across the code, so a tall code in the 25.4 mm print height is more sensitive to that variation than a single-line date at 12.7 mm.
Check before a trial. Is the bottle at room temperature at the print point, or still cold from filling or cold storage? Is there a coating, frosting or label adhesive residue on the print area? Will the bottle be refrigerated, frozen or wiped with alcohol after coding?
How to judge drying. Print, let it dry, then rub-test — and include a cold-store check: print, refrigerate under your normal conditions, then rub-test again. Condensation is the usual failure point in cold-chain use, not the cold itself. If the code must survive handling after cold storage, test that condition specifically; a room-temperature pass does not prove it.
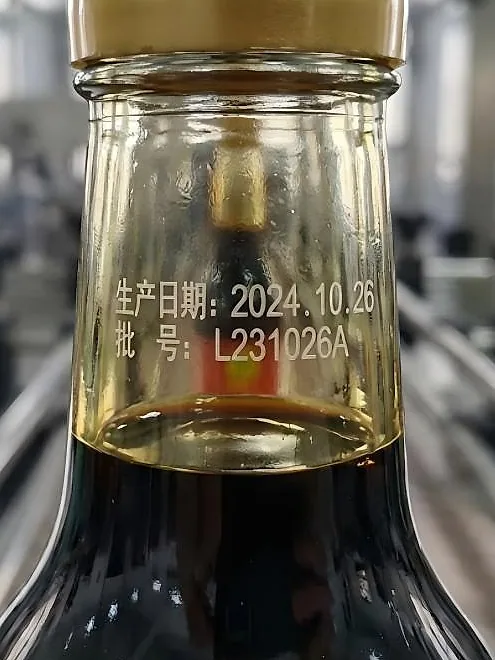
If it fails. Move the print point to after the bottle reaches room temperature, or to before filling, if the line allows it. If neither is possible, say so when you request samples — the primer and ink combination is a sample question, not a datasheet question.
PET and rigid plastic: bottles, containers and caps
PET is the core use case for solvent TIJ, and normally reliable. The exceptions are quiet ones: the bottle looks identical, the cartridge is identical, and the code fails anyway.
What usually goes wrong. Slip agents, silicones and anti-static coatings on the surface. Two seemingly identical bottles from different suppliers can print differently with the same cartridge, because the surface treatment differs. PET measures around 40–42 mN/m, already above the threshold for a solvent ink — but a treated or coated surface is not the PET underneath it.
Check before a trial. Who supplied this batch, and has the surface treatment changed? Is there a silicone or slip additive in the resin or the mould-release process? Is the print area flat, or on a curved shoulder where the throw distance varies? Is the code a single-line date (12.7 mm is enough) or a multi-line block with a QR code (25.4 mm prints it in one pass instead of stitching)?
How to judge drying. PET is the case in the pillar guide: a beverage or cosmetics plant coding production dates on PET bottles, where the aqueous cartridge already used for outer cartons smears on the bottle and the solvent cartridge leaves a bonded code that can be handled soon after the print point. Reproduce that test on your own bottle: print, wait for the first contact point on your line, then rub and scratch lightly. If the product will be refrigerated, frozen or wiped with alcohol, test that condition too — do not assume a room-temperature pass covers it.
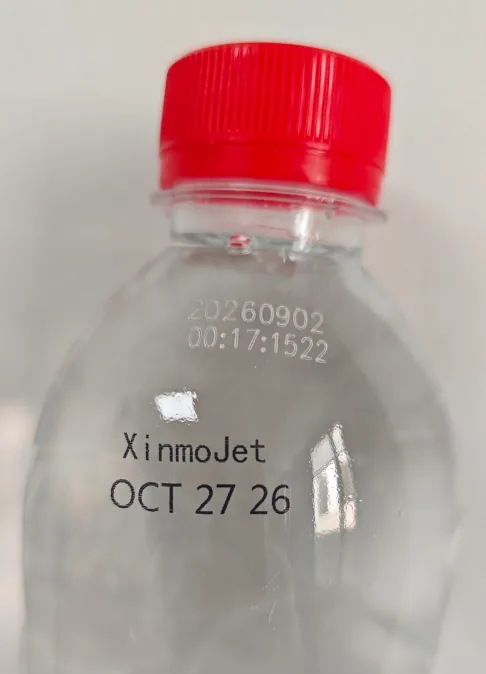
If it fails. Ask the bottle supplier for the current surface treatment before changing cartridges. A coating change at the supplier is a common root cause, and it is cheaper to find out from them than by trialling cartridges.
PE and PP film: pouches, shrink film and labels
PE and PP film are the hardest common surfaces in this guide. Expect to work for the result here; a pass on film is worth more than a pass on metal, because it proves the process, not just the ink.
What usually goes wrong. Low surface energy: untreated PP measures around 26–28 mN/m and HDPE around 28–32 mN/m, both below the surface tension of most coding inks, so a solvent ink can look perfect wet and then flake off under a thumbnail. Corona or flame treatment lifts HDPE to roughly 38–42 mN/m and PP to around 40–44 mN/m — but treatment decays. A treated bottle or film that has sat in a warehouse can fall back below the threshold, so an ink that held in the lab may fail on stock that has been stored.
Check before a trial. What is the current dyne level of this stock — ask your converter, or measure it; do not assume the level from the day it was treated. Is the film moving, fluttering or stretching at the print point? Is the code printed before or after shrink, and does shrinking distort or stress the printed area? For dark film, consider the white ink variant: black ink is invisible on a black cable or dark moulding, and white exists for exactly that contrast problem — that is the whole subject of white solvent ink cartridges.
How to judge drying. The drying budget matters most on film, because film is light, moves, and is often stacked or rolled soon after printing. Note the distance from printhead to first contact and the line speed, and test at that speed — not at a slower trial speed. If the budget is too short, moving the printhead or adding an air knife is usually the fix, not a different cartridge.
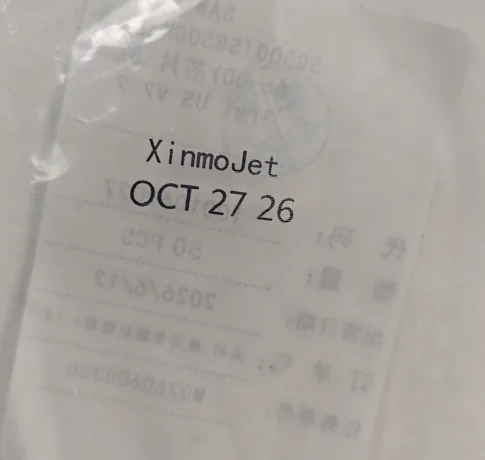
If it fails. Do not keep trialling cartridges against an untreated surface. The answer is usually pretreatment — corona, flame or primer — or a different film specification. Confirm the dyne level on representative stock, not on a freshly treated coupon, and retest after treatment. If the durability target is high enough that a UV-curable system is on the table, that route is compared separately in UV-curable TIJ on PE and PP film — a different ink family, not a variant of this one.
Coated carton: glossy retail boxes
Coated carton sits between the porous and non-porous worlds, and the coating decides which world you are in.
What usually goes wrong. Treating a coated box like a plain carton. A matte coating may still absorb ink; a glossy UV-coated box behaves like plastic. If the coating is unknown, the ink choice is a guess — and a guess is what this trial is for.
Check before a trial. What is the coating — matte, gloss, UV varnish, lamination? Is the print area on the coated face or on an uncoated flap? Will the box be handled, stacked or shrink-wrapped soon after coding, and does it face abrasion in transport?
How to judge drying. Test both ink types on the real box if the coating is unknown, and compare rub resistance after drying — not just appearance while wet. A solvent code on a glossy box and an aqueous code on the same box can look identical wet and behave differently after a rub test. That comparison is the trial.
If it fails. Name the coating when you request samples. “Coated carton” is not a specification; the coating type is. A supplier who asks for it before quoting is a good sign.
A real application: one line, three substrates, one trial method
Consider a food plant that codes three things on one line: a date on a tinplate can lid, a batch number on a glass jar, and a lot code on a PE pouch. Three substrates, one cartridge type, one trial method — and three different failure modes if the trial is skipped.
The can lid fails first on oil: the code wipes off until the sample is cleaned, then holds. The glass jar fails on temperature: the code holds on a warm jar and lifts on a cold-filled one, until the print point moves to after the jars reach room temperature. The PE pouch fails on surface energy: the code flakes until the converter confirms the current dyne level and the film is corona-treated, after which the same cartridge holds.
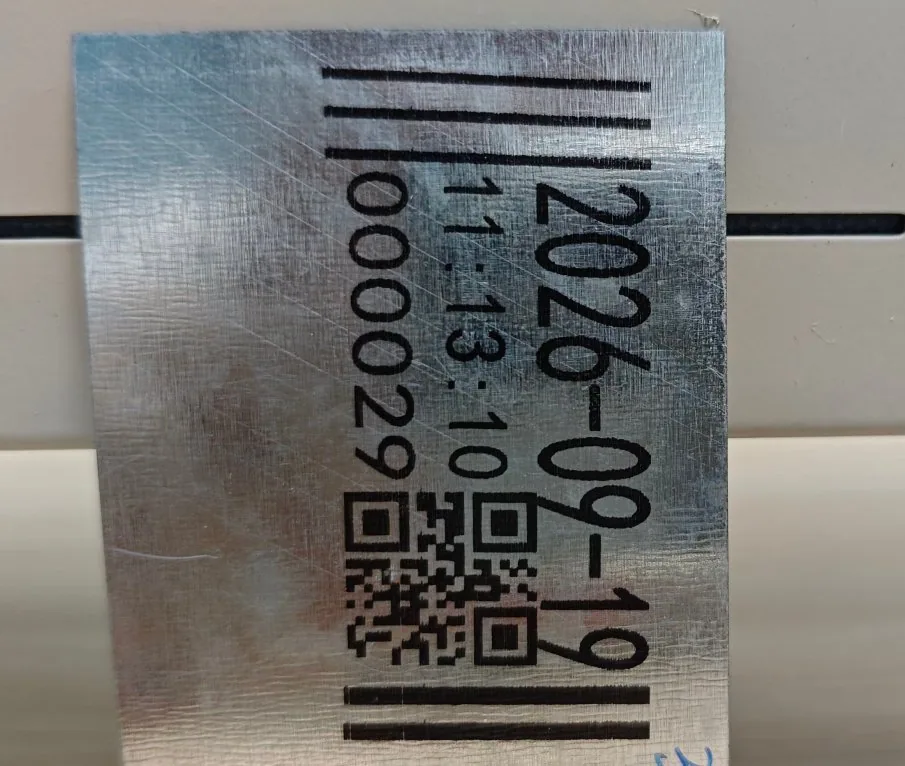
None of the three failures is a cartridge defect, and none is found in a datasheet. Each is found by the method used in every section above: print on the actual product, at the actual line speed, with the actual coding content; tape, wipe and rub test; check the condition the product actually meets; scan with the equipment you use at end of line. That method is the whole guide, applied three times.
The scenario is illustrative — built from a common failure pattern, not measured results. It promises nothing about your can, jar or pouch and puts no number on drying or adhesion for any specific product. It shows the decision path: identify the surface, check what is on it, prove the result on your own product before committing to volume.
When the substrate is not the problem
If every substrate fails the same way, stop changing substrates and check the cartridge and the line instead: printhead distance and stability, idle time between prints, cartridge handling.
Solvent evaporates fast, so it dries inside nozzles that sit open and idle. The product page puts it at roughly 10–15 minutes on fast-dry solvent before the nozzle plate begins to dry — confirm per ink — so lines that print in bursts plan a capping routine or a short purge at restart. Storage and nozzle-care habits are covered in the pillar guide.
If a single substrate fails while the others pass, that is useful information rather than a failed trial: it tells you where the process needs to change — the coating, the treatment, the temperature, the handling — rather than the cartridge. Send those findings with the sample request. The six questions in the pillar guide are the fastest route to a matched sample instead of a generic quotation, and when a code has already failed on the line, a diagnostic order for adhesion failures takes the same job step by step. Sourcing at manufacturer level is on the manufacturer overview, private-label supply on the OEM and ODM programme.
Frequently asked questions
Which substrate is hardest for a solvent TIJ cartridge?
PE and PP film, because of low surface energy. Untreated PP is around 26–28 mN/m and HDPE around 28–32 mN/m, below what most coding inks can wet reliably. Treatment usually lifts them into the workable range, but treatment decays in storage, so test representative stock, not a freshly treated coupon.
Why does my code look fine wet and then flake off?
Because wetting and bonding are different things. An ink can spread evenly while wet and still fail to bond as it dries — the classic sign is a code that looks perfect and then flakes under a thumbnail or lifts with tape. Check the surface first (oil, coating, treatment level), then run a tape test rather than judging by appearance.
Does a solvent TIJ cartridge work on glass without a primer?
Sometimes, and it depends on the glass, the primer and the conditions — glass is chemically inert, so adhesion often depends on a primer rather than on the ink alone. Test on your own bottle, including a cold-store check if the product is refrigerated, and do not treat a room-temperature pass as proof for a cold-filled line.
How do I know if drying is fast enough for my line?
Measure the distance from the printhead to the first thing that touches the code, and your line speed — those two numbers are the drying budget. The typical band is 1–5 seconds on non-porous surfaces, but the test is whether the code survives first contact, stacking and handling on your line, not whether it looks dry in the air.
Can I use the same cartridge for metal, glass and plastic?
Often yes — the XM-45S is specified for HDPE, LDPE, PP, PET, rigid PVC, coated metal and metallised film, and glass — but “same cartridge” does not mean “same result without a trial”. Each substrate needs its own sample test, because the failure mode is different for each one. The full specification is on the solvent ink cartridge range page.
What should I send a supplier to get a useful sample?
The material and finish, the line speed, the code content and height, what the code must survive, and the distance to first contact after printing. With those, a supplier can match an ink and print height — 12.7 mm or 25.4 mm — instead of quoting a generic cartridge. Use the contact page to describe your surface and line conditions.
Summary: the surface decides, the trial proves it
Metal forgives a dirty surface least once it is clean; glass punishes cold and condensation; PET punishes a changed surface treatment; PE and PP film punish low surface energy and decaying treatment; coated carton punishes anyone who guesses the coating. The cartridge is the same in all five cases. The trial is what differs — and the trial is what turns a specification into a code that is still readable when your customer opens the box.
Choose in this order: name the exact material and finish, check what is on the surface, confirm the drying budget on your line, print on your own product at your own speed, and judge with a tape, wipe and rub test plus a scan. That is the whole guide, and it is the same method the substrate matching guide sets out in engineering terms. Current pricing and order quantities are on the pricing page.
Related reading
- 26 October 2026
What Is a Solvent TIJ Cartridge? Complete Guide for Non-Porous Coding
A solvent TIJ cartridge is a 42 ml thermal inkjet cartridge filled with a fast-drying solvent ink, built for m…
- 30 October 2026
How Solvent TIJ Cartridges Are Made: Inside a Manufacturer's Line
A solvent TIJ cartridge is not bought parts relabelled. It is ink formulated and filtered, a body prepared and…
- 29 October 2026
How Much Does a Solvent TIJ Cartridge Really Cost? Cost per 1,000 Prints
USD 28–58 buys a solvent TIJ cartridge, and that number decides nothing. What reaches your margin is the cost …
Want this confirmed on your own material?
We print on samples of your actual substrate and send them to you. Send the material, the line speed and the code content, and we will tell you honestly whether the fault is the ink, the surface or the line layout.